What the siRNA manufacturing model for peptide production can and cannot borrow
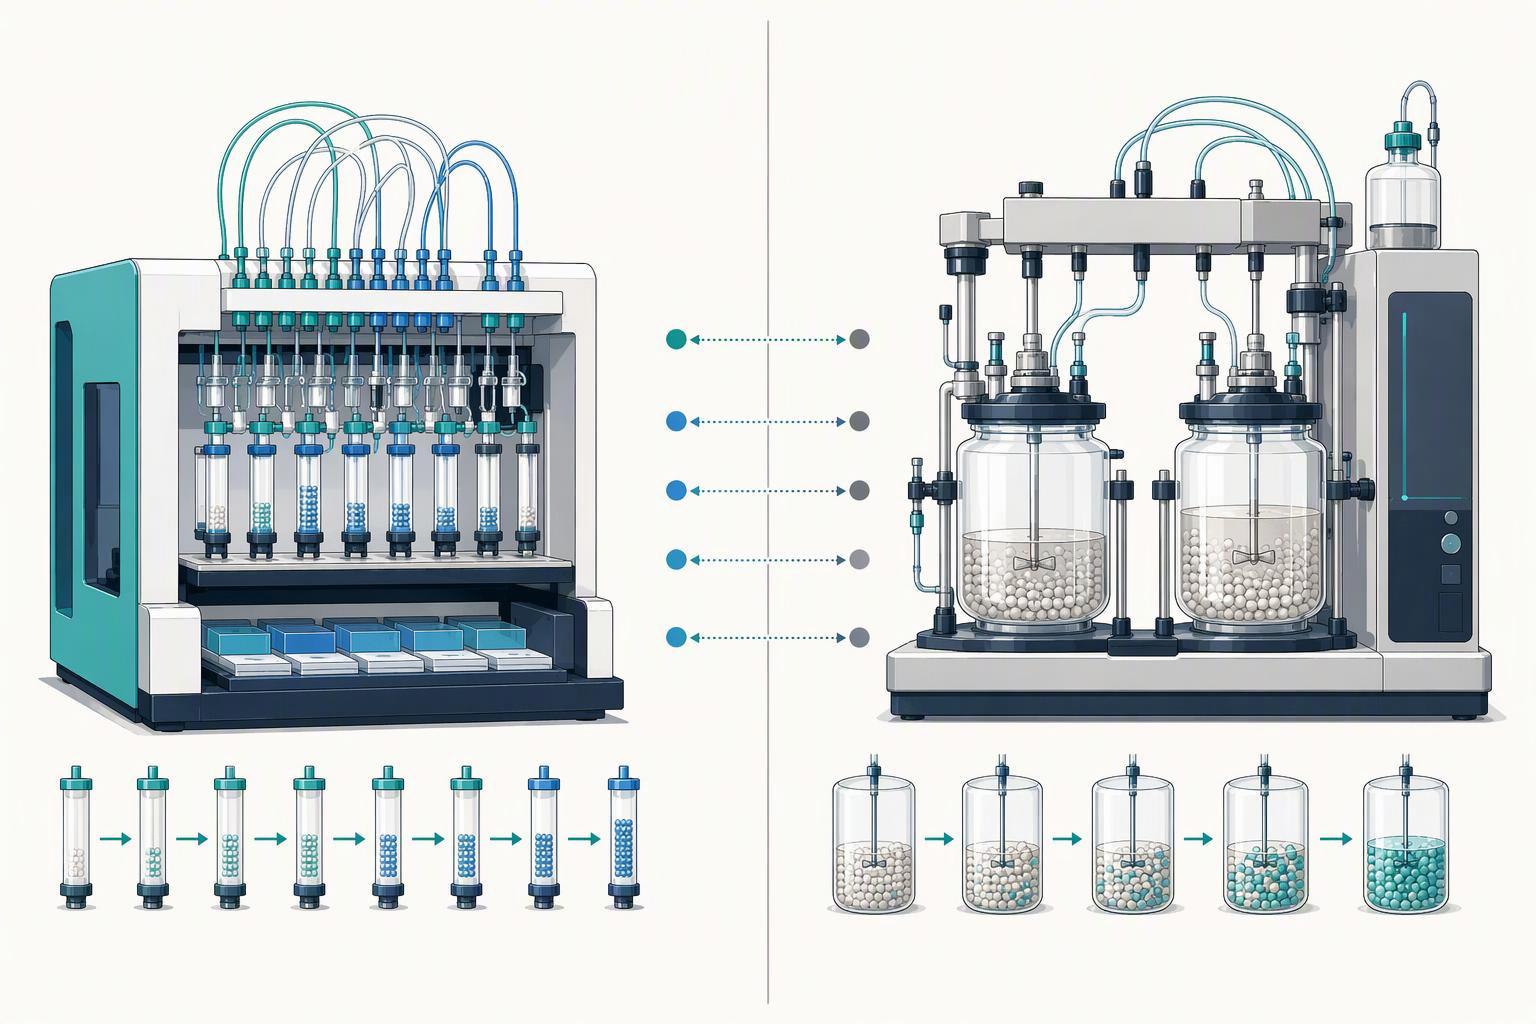
If your peptide program has reached the point where scale-up and impurity burden have outgrown bench practice, the siRNA manufacturing model for peptide production is worth reading carefully, and worth reading skeptically. Bachem’s disclosed fragment-and-ligation case study describes building short RNA fragments and joining them enzymatically rather than assembling one long chain, with the stated economic rationale of fewer and simpler downstream purification steps, lower solvent use, less waste and lower cost of goods at gram to multi-kilogram scale (Bachem, retrieved 2026-09-21).
Fragment-and-ligation means synthesizing defined pieces separately and then joining them, instead of growing one continuous chain. An n-1 shortmer is a chain missing one residue, and racemization is the loss of a chiral center’s intended configuration, both of which become harder to control as chains lengthen. Fit-for-purpose analytics means testing matched to what a decision needs, not to a fixed panel.
This is an interpretation of public material, not a peptide recipe. Nucleic-acid manufacturing versus peptide chemistry involves different coupling, protecting-group and stereochemistry problems, so the transferable part is process design, not chemistry.
What Bachem’s disclosed siRNA route actually describes
Bachem’s disclosed fragment-and-ligation case study, run with Codexis and using vutrisiran as the model siRNA, describes building the molecule from short RNA fragments that are synthesized separately and then joined enzymatically. The company reports that this route can “achieve high ligation efficiencies, simplify purification, and support multi-kilogram GMP production,” with product quality it describes as comparable to conventional synthesis (Bachem case study, retrieved 2026-09-21).
Bachem’s own framing of enzymatic ligation gives the economic rationale: joining short fragments rather than building one long chain offers “higher yields and reduced purification burdens,” particularly at large quantities (Bachem knowledge center, retrieved 2026-03-24).
Two limits matter. This is a vendor’s self-report: the pages state no yield, purity or cost figures, so the efficiency and cost-of-goods claims cannot be checked against published numbers. And the disclosure sits inside a broader positioning, since Bachem’s oligonucleotide manufacturing page presents it as a partner across both peptides and oligonucleotides, with a dedicated GMP oligonucleotide site and first GMP batches within nine months of kick-off (Bachem oligonucleotide NCE page, retrieved 2026-07-30).
Where the analogy breaks
The two manufacturing logics diverge at the chemistry itself. Oligonucleotides are built nucleotide by nucleotide from 5′-DMT-protected nucleoside-3′-phosphoramidites, cycling through detritylation, coupling, oxidation or sulfurization, and capping. Peptides are built amino acid by amino acid by Fmoc or Boc solid-phase synthesis, with iterative deprotection and coupling. The side-by-side chemistry comparison in RSC Green Chemistry’s 2023 review notes the two routes are not directly compatible without special protecting-group design.
The impurity taxonomies differ just as sharply. The FDA’s oligonucleotide analytical thinking describes oligonucleotide impurities as chain-length species (shortmers, longmers, n-1) and phosphorus-stereochemistry variants such as phosphorothioate diastereomers, with full-length and near-full-length species that chromatography does not remove. The EMA guideline on synthetic peptides instead centers deletions, truncations, racemization, over- and under-coupling, dimers and aggregates, and residual reagents, solvents and counterions.
|
Dimension |
Oligonucleotide synthesis |
Of Peptides Peptide SPPS |
|---|---|---|
|
Building block |
5′-DMT nucleoside-3′-phosphoramidite |
Fmoc- or Boc-protected amino acid |
|
Cycle |
Polypeptide Production Detritylation, coupling, oxidation/sulfurization, capping |
Deprotection, coupling, Preparation Of Peptides wash |
|
Dominant impurities |
Shortmers, longmers, n-1, phosphorothioate diastereomers |
Deletions, truncations, epimers, aggregates, counterions |
|
Hard-to-remove species |
Full-length and near-full-length impurities |
Sequence-dependent aggregates |
Peptides also carry chiral centers absent from the nucleotide backbone, and aggregation is sequence-dependent rather than predictable. તરીકે peptide.com’s SPPS side-reaction reference explains, resin aggregation causes incomplete deprotection and coupling, is signalled by failure of the resin to swell, and cannot be predicted reliably from sequence, though hydrophobic sequences are more prone and it is unlikely before residue 5-6 or after residue 21.
Four principles that do transfer
Four things carry over from oligonucleotide manufacturing: modular process design for peptide synthesis, mechanism-level impurity control, staged scale-up planning, and fit-for-purpose analytics for peptide manufacturing. Each is a principle, not a copied protocol. Solid Phase Organic Synthesis
Modular process design. The available building-block toolbox already includes standardized protected amino acids, pseudoprolines and Dmb or isoacyl dipeptides, alongside deliberate resin and linker selection (Merck/Novabiochem). Module-based plants reuse qualified blocks to add capacity with lower qualification risk.
Impurity control at the mechanism. Control what generates the impurity, not the peak on the chromatogram. The SPPS side-reaction reference lists mitigations that transfer as principles: DBU deprotection, NMP or DMSO cosolvent, higher coupling temperature, and hydrogen-bond-disrupting elements such as pseudoprolines and Hmb or Dmb backbone protection (peptide.com, 2019-10-14).
Scale-up planning. Confirm route behavior, impurity trend, and downstream performance at small scale before committing to larger equipment. The exponential yield-decay relationship explains why: ખાતે 99% જોડાણ કાર્યક્ષમતા, full-length yield falls to roughly 82% after 20 couplings, 67% after 40, અને 45% after 80 (Peptides Codex, 2026-09-14).
Fit-for-purpose analytics. ICH Q2(R2) validation expectations cover specificity and discrimination, precision, ચોકસાઈ, linearity and range, robustness, and a quantitation limit at or below the reporting threshold; where authentic impurities are unavailable, specificity may be shown with a second well-characterized orthogonal procedure (ICH Q2(R2), 2023-11-30, error correction 2025).
What this means for peptide developers, CDMO selection and program timelines
For peptide developers, the four principles change one thing above all: peptide impurity control and scale-up planning become a control-strategy problem rather than a purification problem. ICH Q11’s control-strategy expectations require a science- and risk-based strategy that justifies starting-material specifications, controls starting-material impurities, and demonstrates process reproducibility against predefined quality attributes. Applied to a peptide route, that means impurity trends are tracked from route confirmation onward, not discovered at release testing.
For CDMO selection, the same logic converts into questions rather than claims. Ask a candidate to describe the staged supply-agreement structure it uses: small-scale technical confirmation first, impurity trend data second, downstream performance third, commercial પેપ્ટાઇડ સંશ્લેષણ scale last. CDMO-practice disclosures, including Polypeptide Group’s strategy reporting and the 2026 DCAT CDMO review, describe this staged pattern as the norm for long-term agreements, which is why it works as an evaluation lens rather than a vendor promise.
Timelines follow from that staging. A program that confirms route and analytics before committing to commercial scale absorbs more cost early and less rework later; one that skips confirmation compresses the front end and pays at scale-up. Ng Peptides
ટીપ માટે: Ask for the staged confirmation plan in writing before signing. MOL Changes supports this kind of front-loaded planning through process development and scale-up services, from milligrams to kilograms.
Next steps
If the transferability question is now the live one for your program, the useful next step is a technical feasibility assessment rather than a commercial conversation. Ask for documentation covering three things: route-confirmation data for the sequence you actually intend to scale, impurity-profile reporting that shows how the profile is tracked across batches rather than reported as a single release number, and the release-testing documentation behind the analytical methods. Those three items let your CMC team judge fit before any supply commitment is discussed.
MOL Changes provides custom peptide synthesis, process development and quality control for programs moving from milligrams to kilograms, and can supply that documentation package on request.
વારંવાર પૂછાતા પ્રશ્નો
Does fragment-and-ligation chemistry actually apply to peptides?
Partly, and the distinction matters. Native chemical ligation and its variants were developed for peptide chemistry before oligonucleotide synthesis borrowed the concept, so the underlying idea is not foreign to peptides at all. What does not carry over is the scale of the win. The side-by-side chemistry comparison shows that oligonucleotide assembly gains far more from switching to a modular route than peptide assembly does, because peptide couplings already run at high efficiency on solid support. Treat ligation as a targeted tool for sequences that resist stepwise synthesis, not as a replacement platform.
We have already committed to a conventional SPPS route. What changes?
Nothing about the chemistry, and a great deal about the planning. The available building-block toolbox for peptides is already broad, so the practical move is to keep SPPS and apply the modular thinking to how you stage development: confirm the route early, track impurity trends as a distinct workstream, and defer scale commitment until the trend is stable. Programs that treat impurity control as a late-stage cleanup problem rather than a running measurement tend to discover the hard numbers at the worst possible time.
How much analytics work is genuinely necessary?
More than most early programs budget for, and less than a fully validated commercial panel. ICH Q2(R2) validation expectations give you the framework: decide which methods are stability-indicating and which are merely in-process checks, then validate each to the standard its decision actually requires. Running a full release panel on every in-process sample is overengineering. Running nothing until the first scale batch is the opposite mistake.
The transferable elements are staged route confirmation, impurity tracking and defined analytical decisions. RNA fragment preparation and enzymatic ligation involve different substrates, enzyme requirements and impurity mechanisms from peptide synthesis. Demonstrate a peptide-specific route before borrowing process-efficiency or scale-up claims.
નિષ્કર્ષ
The siRNA model’s value to peptide production is architectural, not chemical. What transfers is the discipline of confirming a route in stages, controlling impurities at the mechanism level, and matching analytics to the decision they inform. What does not transfer is the synthesis chemistry itself, and any plan that treats oligonucleotide process knowledge as directly portable will misallocate effort.
If staged confirmation and mechanism-level impurity control become normal practice in peptide programs, the practical effects show up in three places. Developers stop discovering late that a route cannot hold its impurity profile at scale. CDMO selection shifts from comparing headline purity numbers to comparing how a supplier confirms a route before committing to it. Program timelines absorb more cost early and less rework later, which is a better trade for any peptide heading toward commercial supply.
The next step is not a technology decision. It is a scoping one: before the next scale-up campaign, write down which impurities your current route can and cannot control, and at what point in the process you would know. That list is what makes a technical feasibility conversation useful, whether you have it internally or with a manufacturing partner.